What Is CNC Press Brake Programming?
Programming connects the finished drawing to a sequence of bends, tool stations, positioning references and corrections. The program belongs to a defined machine and setup. Reusing a file on another machine, with different tooling or after a drawing revision requires a compatibility review.
Delem DA66T vs DA69T: Controller Comparison
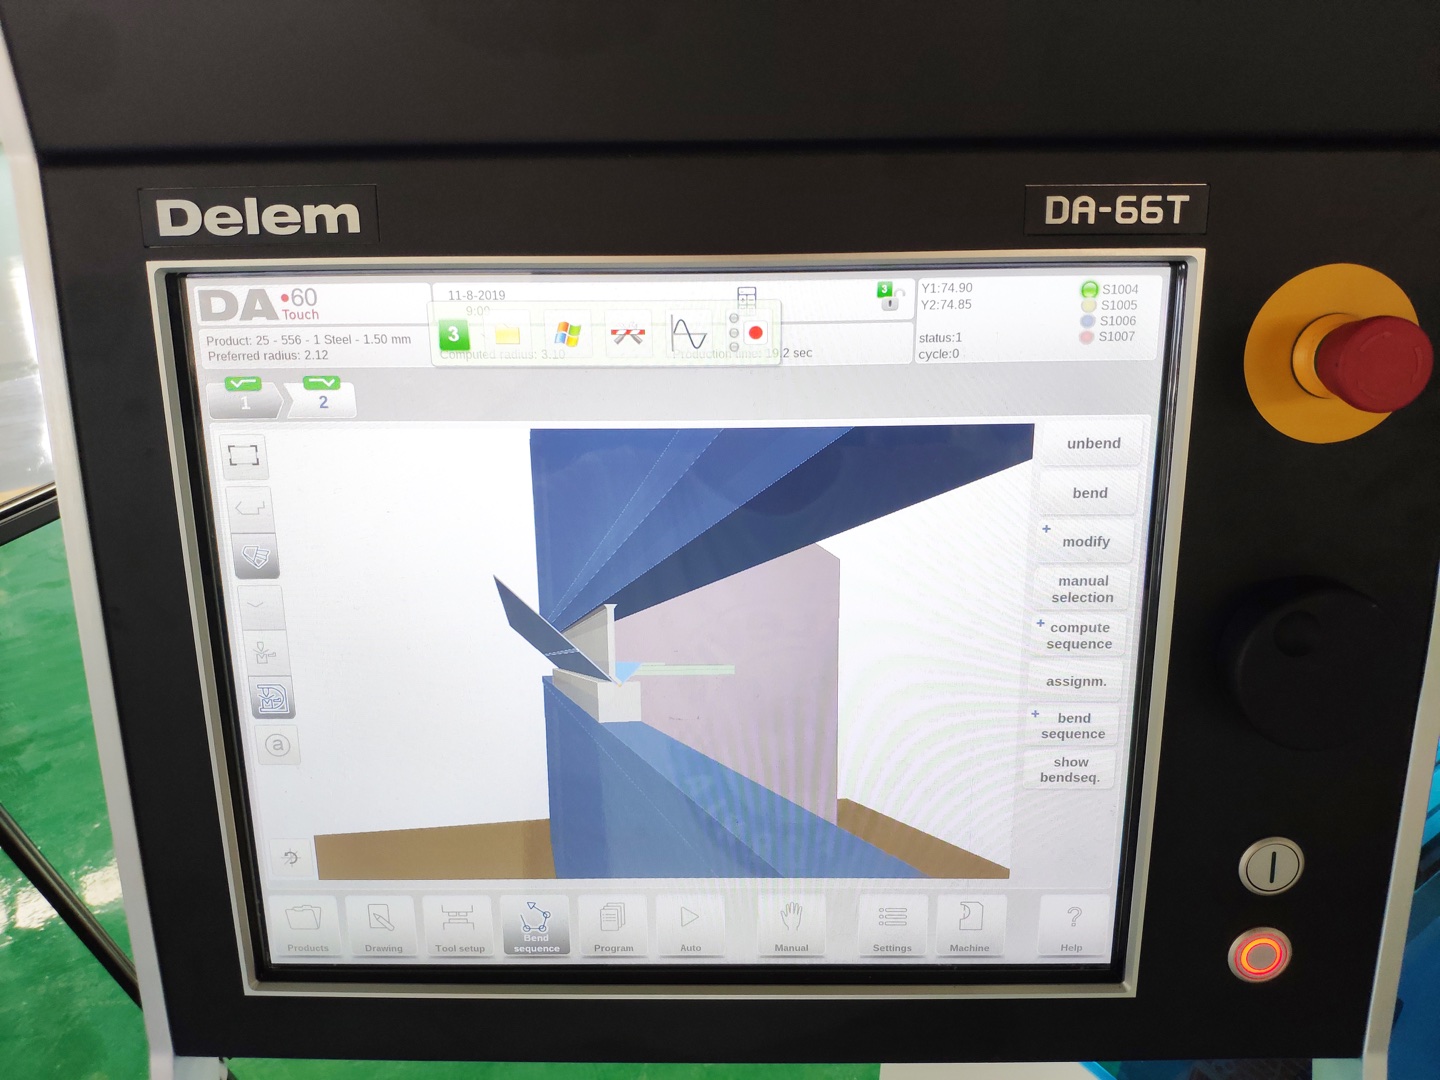
Delem's published specifications distinguish the following functions. These are controller-family references; ask the machine supplier to confirm the installed version, enabled options and quoted software package.
| Function to distinguish | Delem DA-66T | Delem DA-69T |
|---|---|---|
| Graphical programming | 2D graphical programming | 2D and 3D graphical programming |
| Published display size | 17-inch touchscreen | 17-inch touchscreen |
| Sequence and collision review | Automatic bend-sequence calculation and collision detection; 3D machine setup is described by Delem. | Automatic bend-sequence calculation and collision detection; 3D visualization in simulation and production is listed. |
| Listed offline software | Profile-TL | Profile-T3D |
Primary references, reviewed October 31, 2026: Delem DA-66T · Delem DA-69T · Delem Profile-T
Which Profile-T edition is included?
Delem lists Profile-TL, Profile-T2D and Profile-T3D. Its current Profile-T page assigns DXF import to Profile-T2D and above, and 3D CAD import to Profile-T3D. Specify the edition, license, compatible control version, machine model and transfer workflow in the quotation; the phrase 'offline programming included' leaves these questions open.
CNC programming to press brake specification matrix
Use this review record to connect a programming requirement to supplier evidence. It is a procurement checklist, not a machine setup sheet.
| Input to provide | Evidence to request |
|---|---|
| Representative part drawing and CAD format | Demonstration of the required import, bend-sequence and visualization functions with the quoted software edition. |
| Punches, dies, holders, adapters and station layout | Matching tool-library geometry, clamping compatibility, clearances and applicable load limits for every component. |
| Bend length, return flanges and finished-part removal | Machine geometry, back gauge travel and finger arrangement; review all bends and removal with the actual configuration. |
| Material grade, thickness and finished tolerances | Agreed trial material, inspection method and acceptance criteria. A controller model is not an accuracy guarantee. |
| Part mix, program reuse and office preparation | Software license scope, backup and transfer method, operator training and responsibility for maintaining machine/tool data. |
Understanding Press Brake Axes
On configurations using these labels, Y1/Y2 identify left and right ram control; X is back gauge depth, R is height, and Z1/Z2 position the fingers laterally. Independent X1/X2 is a separate configuration question. Ask for the actual axis list and crowning arrangement instead of inferring them from a controller's maximum capability or an advertised total axis count.
Back gauge axes and configuration
Step-by-Step CNC Press Brake Programming (Delem DA Guide)
The following steps organize program preparation and review. Startup, homing, calibration, safeguarding and machine operation require the builder's instructions and trained personnel; generic menu paths or speed values cannot replace them.
1. Freeze the drawing and material record
Identify the part revision, bend datums, thickness, material condition and finished tolerances. Record rolling direction where relevant and keep it separate from cosmetic finish direction.
2. Match the machine and tooling data
Confirm the machine model, axes, punch/die geometry, holders and adapters. Review support, clearance and rated loads before relying on the software model.
3. Define the bend sequence and references
Document bend identifiers, positioning faces, tool stations and handling requirements. Check access to the gauge reference after each preceding bend.
4. Review the simulated configuration
Check the modeled part, machine, tools and gauge fingers against the proposed setup. Review intermediate geometry and part removal. Resolve missing or approximate geometry before accepting the simulation.
5. Evaluate a representative first piece
Arrange an approved trial under the machine builder's procedures. Record measured angles, flange dimensions and other drawing requirements, then review corrections using the installed control's conventions.
6. Release a traceable program revision
Retain the accepted drawing, machine/tool configuration, material record, inspection results and program revision together. Review substitutions before reusing that approval.
Press Brake G-Code: What You Need to Know
Do not assume that a generic G-code example or file extension is accepted by a particular press brake. Confirm the supported format and transfer procedure for the installed control and software. Keep angular values separate from linear axis positions: a target angle in degrees is not a Y-axis position in millimeters.
Springback Compensation in CNC Programming
Evaluate the unloaded result for the actual material and tooling. Confirm whether the control expects an included angle, bend angle or correction value before changing a program. There is no universal springback offset or back gauge correction for every job. A change between air bending, bottoming and hemming needs a separate tooling and load review.
5 Common CNC Press Brake Programming Mistakes to Avoid
- Treating 2D programming as proof that collision review or 3D machine visualization is unavailable.
- Assuming every offline software edition imports the same CAD formats or is included in the machine price.
- Using nominal controller capabilities as proof of the machine's installed axes, accuracy or tool capacity.
- Reusing a generic die-opening multiplier, speed, springback angle or flange-offset formula as an approved setup.
- Releasing production from a simulation alone without checking model accuracy, handling and representative first-piece results.
Frequently Asked Questions
Does the Delem DA66T support 3D simulation and offline programming?
Delem describes 2D programming, collision detection and 3D machine setup for DA-66T, and lists Profile-TL offline software. Distinguish these functions from 3D product programming; confirm the installed options and offline edition with the supplier.
What should be specified when buying a press brake with a DA66T system?
Specify representative parts, material, bend length, tolerances, actual axes, tooling and clearance requirements. Itemize offline software, enabled options, training and the acceptance trial in the quotation.
What is the standard programming unit for CNC press brakes?
Confirm the selected unit system and each field's meaning in the installed control. Distinguish angles, linear positions, speeds and forces; do not enter a degree value into a linear Y-axis field.
How long does it take to program a CNC press brake?
Time depends on geometry, available machine/tool data, software functions and the review required. Evaluate a representative part; a generic minute estimate does not include every setup, handling or first-piece check.
Can CNC press brake programs be saved and reused?
Use the backup and transfer functions supported by the installed system. Before reuse, check the drawing revision, machine configuration, tooling, material and approved corrections. A saved filename alone does not prove compatibility.
What is the difference between air bending and bottoming in CNC press brake programming?
They use different forming conditions and require the corresponding tool data, program settings and load assessment. Do not reuse an air-bending program or apply a generic force multiplier to approve bottoming.
What press brake machine specification is needed for reliable CNC programming?
Match the actual machine geometry, axes, tooling, support and software to representative parts. Confirm applicable limits and acceptance criteria with the supplier; no controller name guarantees a finished tolerance.
CNC press brake programming quote checklist
Send Rucheng the drawing revision, material and thickness range, bending length, tolerances, CAD format and expected part mix. Request an itemized machine, tooling, software and training proposal, with configuration and acceptance conditions confirmed before ordering.
Send press brake quote requirements