
Before Ordering Press Brake Dies: Fit, Clearance and Load
- Clamping fit: send the punch tang and die-base drawings or dimensions, holder details and machine model. A similar tool profile does not establish compatibility.
- Part clearance: check the bend sequence, return flanges, tool heights, adapters and available opening. Confirm that the formed part can be removed and specify the required segment lengths.
- Load limits: check the punch, die, holders and machine. A short segment cannot carry the full load quoted per metre. Follow the supplier's loading conditions, not just the machine's total tonnage.
Compare press brake molds and dies, review the bending force calculation, or send your tooling details for a press brake tooling quote.
What Is Press Brake Tooling and How Does It Work?
Press brake tooling combines an upper punch and a lower die on a press brake machine. The punch applies force while the die supports the sheet. Tool geometry, material properties and the bending method together determine the resulting bend.
Selecting the correct tooling is one of the most critical decisions in sheet metal fabrication. The wrong punch-die combination leads to inaccurate angles, surface damage, excessive tonnage, or even tool breakage. Understanding the full range of available tooling types — and when to use each one — separates efficient production shops from those wasting time and material on trial-and-error bending.
This guide covers every major type of press brake punch and die, explains when and why each is used, and provides practical selection guidelines including the critical V-die opening width formula that determines bend quality.
Press Brake Punches (Upper Dies): Types and Applications
The punch is the upper tool that descends into the die, applying force to the sheet metal. Different punch profiles produce different bend geometries and provide clearance for various part shapes. Here are the most common types:

Standard Punch (Straight Punch)
The standard punch has a symmetrical V-shaped tip with a relatively thick body. It is the workhorse tool for general-purpose bending operations, including air bending, bottom bending, and coining. Standard punches typically have tip angles of 85° or 88° (slightly acute) for air bending, allowing the operator to achieve exact 90° bends by controlling the punch depth.
Straight punches suit simple L-bends and brackets when the tool body clears the part. Their usable thickness range depends on the specific punch, die opening, material and load limits; it cannot be inferred from the profile name alone.
Gooseneck Punch (Swan Neck Punch)
The gooseneck punch is one of the most important specialty tools in any press brake shop. Its defining feature is a deep, curved or offset profile that provides clearance for previously formed flanges or box walls. Without a gooseneck, the workpiece would collide with the punch body when making the second, third, or fourth bend on a multi-bend part.

Best for: U-channels, C-channels, box profiles, J-bends, Z-bends, and any part with return flanges that would interfere with a straight punch. Gooseneck punches are available in various throat depths — the deeper the throat, the taller the flange it can clear, but the lower the maximum tonnage rating due to the reduced cross-section at the neck.
⚠️ Gooseneck Tonnage Warning
Check the load rating for the exact gooseneck profile, segment and holder. A deeper relief changes clearance and strength; do not infer capacity from punch height or a generic model number. Confirm load units and permitted loading conditions with the supplier.
Acute Angle Punch
Acute angle punches have a narrow, sharply angled tip designed for bending angles less than 90° — typically 30° to 60°. They are essential for hemming operations (the first step is an acute pre-bend before flattening), and for decorative or functional parts requiring sharp angles. The narrow tip also makes them useful for bending very short flanges where a standard punch body would interfere.
Best for: Pre-bends for hemming (typically 30° acute bend), sharp angles on architectural metalwork, offset bends, and short flanges under 10 mm where clearance is limited.
Radius Top Punch
Instead of a sharp V-tip, the radius top punch has a rounded nose with a specific radius (e.g., R5, R10, R20 mm). It is used to create smooth, curved bends rather than sharp corners. Radius punches work with standard V-dies — the combination of the rounded punch and V-die opening determines the final bend radius.
Best for: Architectural panels, decorative elements, tube-like profiles, parts where a smooth radius is specified on the drawing, and applications where sharp bends would crack the material (common with aluminum and high-strength steel).
Sash Punch
The sash punch has a very narrow, flat body with the tip offset at an angle. This design provides clearance similar to a gooseneck but in a different orientation — the narrow profile allows the punch to fit into tight spaces and bend around corners that would be inaccessible with thicker tooling.
Best for: Window frame profiles, narrow channel sections, and parts with complex multi-bend geometry where standard punches cannot physically fit.
Offset Punch (Joggle Punch)
Matched offset punches and dies can form opposing bends in one stroke. The tool geometry defines the nominal offset. Confirm material thickness, load, part clearance and achievable tolerances with the supplier; the tool does not guarantee perfectly symmetric finished angles.
Best for: Z-profiles, step flanges, overlap joints, panel stiffeners, and any part requiring two parallel bends at a fixed distance.
Press Brake Dies (Lower Dies): Types and Applications
The die is the lower tool that supports the workpiece and defines the bend geometry together with the punch. The die opening width, shape, and angle are the primary factors controlling bend radius, bend angle, and required tonnage.

Single V-Die
A single V-die has one V-shaped groove. Check the opening width, groove angle and shoulder radius against the part requirements and the tooling supplier's data.
Single V-dies are available in standard angles of 30°, 60°, 85°, 88°, and 90°. For air bending — the most common bending method — an 85° or 88° die is standard because the material springs back slightly after the punch retracts, and the slightly acute die compensates. For bottom bending (bottoming), the die angle must match the desired final bend angle exactly.
Multi-V Die (4-Way Die)
A multi-V die has multiple V-grooves of different widths machined into a single die block, typically on 2 or 4 sides. By rotating the die block, the operator can quickly switch between different V-opening widths without removing the die from the machine. This dramatically reduces changeover time for shops processing mixed thicknesses.
Before changing a multi-V opening, follow the machine and tool supplier's handling procedure. Verify the active groove, clamping, alignment and programmed geometry afterward. Changeover time depends on tool weight, holders and handling equipment, not a fixed number of seconds.
💡 Multi-V Die Tip
After changing a multi-V die opening, check tool seating, alignment and the programmed tool geometry. Automatic recognition or adjustment requires compatible tooling, sensors and machine integration; a controller model alone does not guarantee it.
Two-V Die
A two-V die offers two V-openings. Two grooves do not imply automatic centering. Confirm the holder interface and follow the tooling supplier's alignment and clamping instructions.
Hemming Die (Flattening Die)
Hemming is a two-step process: first, an acute angle bend (typically 30°) is made with a standard or acute die; then, the hemming die flattens the acute bend completely, folding the metal back on itself to create a smooth, doubled-over edge. Hemming dies have a flat surface with a slight relief groove that accommodates the folded material.
Best for: Door panels, automotive body panels, appliance enclosures, and any product where a safe (no sharp edge), reinforced, or aesthetically clean edge is required. Hemmed edges also increase part rigidity.
Spring-loaded hemming tools can combine pre-bending and flattening in one setup, but these remain separate forming stages. Reposition the part as the tool instructions require and assess hemming force separately from ordinary bending. See WILA hemming guidance.
U-Die (Channel Die)
U-dies have a U-shaped channel that creates a complete U-bend in a single stroke — both sides bend simultaneously. This is faster and more accurate than making two separate V-bends. U-dies are manufactured to specific widths and depths, so each die works for one particular channel dimension.
Best for: Cable trays, drainage channels, structural C-channels, appliance rails, and any uniform U-profile produced in volume.
Z-Die (Offset Die)
Z-dies create two bends simultaneously at a fixed offset distance, producing a Z-shaped or S-shaped step in the material. This is used for lap joints, panel offsets, and step flanges. The alternative — making two separate bends — requires repositioning the workpiece and risks cumulative angle errors.
Radius Die
Large-radius parts may use dedicated radius tooling or a sequence of smaller bends. There is no universal R25 cutoff requiring a special die. Compare surface quality, contour tolerance, springback and tool clearance. See WILA large-radius bending guidance.
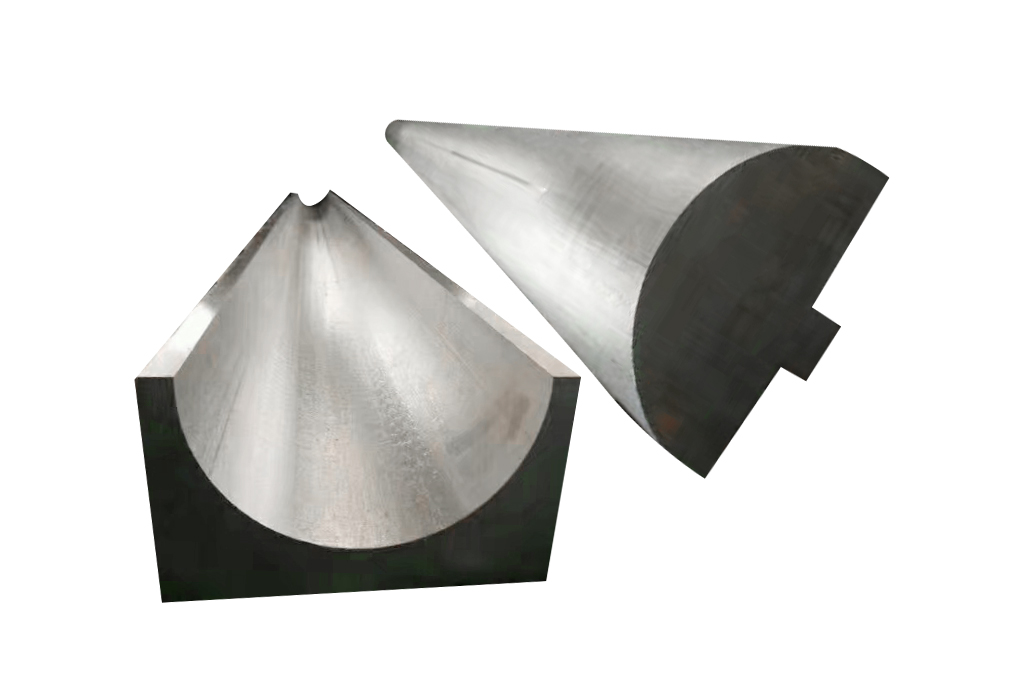
Best for: Curved architectural panels, cylindrical segments (tank shells), elliptical profiles, and decorative metalwork where a smooth radius is essential.
How to Select the Right V-Die Opening Width
For air bending mild steel sheet up to about 3 mm, 6-8 times thickness is a starting range, not a universal die specification. See WILA V-opening guidance. Confirm the actual material, bend angle and tooling before production.
| Material Thickness (mm) | Starting V-opening range (mm) |
|---|---|
| 1 | 6-8 |
| 1.5 | 9-12 |
| 2 | 12-16 |
| 3 | 18-24 |
These ranges are calculated from 6-8 times thickness; they are not a list of stocked dies. Select an available opening only after checking the required inside radius and minimum flange length.
Do not apply this thin mild-steel example directly to thick plate, stainless steel or aluminum. Check grade, temper, rolling direction and bendability. Review the bend radius guide and verify the first part.
Use the bending calculator for a preliminary force estimate, not an exact machine setting. Confirm material strength, bend length and V-opening, then check machine, punch, die and holder limits with the supplier.
Air Bending vs Bottom Bending vs Coining: How Tooling Differs
The bending method determines how the punch and die interact with the material, and different methods have different tooling requirements:
| Method | How It Works | Tooling Requirements |
|---|---|---|
| Air Bending | Punch pushes material into die without touching die bottom; angle controlled by depth | One punch+die set produces many angles |
| Bottom Bending | Punch presses material firmly into die; material conforms to die angle | Die angle must match target angle; needs matched sets |
| Coining | High pressure plastically forms the material against matched tooling; verify process and load limits | Matched punch+die at exact angle; highest tooling cost |
Select the bending method with the tooling supplier. Check the tool angles, material, machine limits and target tolerances. Air bending offers angle flexibility within the tooling geometry; bottom bending and coining require a separately verified setup and load assessment.
Press Brake Tooling Materials: What Your Dies Are Made Of
A steel grade alone does not specify tool performance. Request the grade and applicable standard, heat-treatment method, surface hardness and hardened depth, dimensional tolerances and load rating for the quoted tool. Do not assume different national grade names are interchangeable.
There is no universal cycle-life figure for a die or protective insert. Inspect condition and bend results at the supplier-recommended intervals, and stop using damaged tooling. See WILA damage and wear guidance.
For Rucheng press brake tooling, request a model-specific specification and quotation. Confirm material, heat treatment, compatible holders, segment lengths and any custom profiles in writing before ordering.
Mark-Free (No-Scratch) Tooling: Protecting Surface Finishes
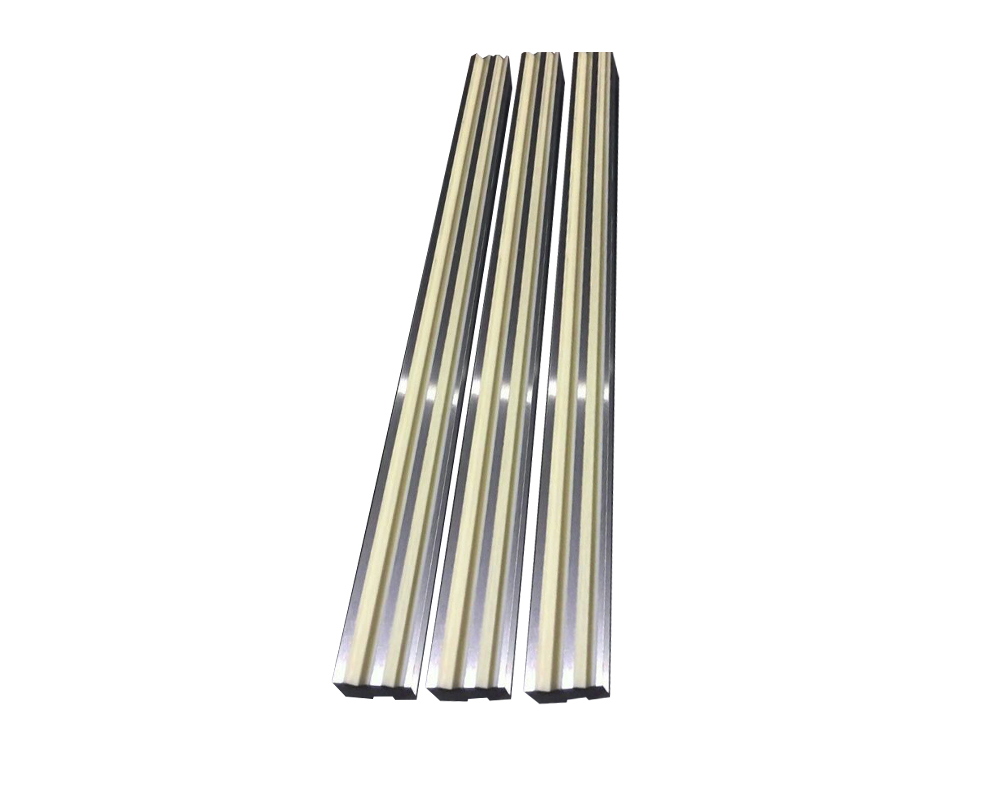
Standard steel dies leave witness marks (die lines) on the workpiece surface where the material contacts the die shoulders. For most structural work, this is acceptable. But for pre-painted, polished, brushed stainless, or visible architectural parts, these marks are a quality reject.
Mark-free tooling uses replaceable urethane (polyurethane) or nylon inserts on the die shoulders that cushion the material during bending. The inserts distribute the bending force without scoring the surface. Urethane inserts are available in different durometers (hardnesses) — softer for thin, delicate materials; harder for thicker sheets that need more support.
Use surface-protection tooling when finish requirements justify it. Test on the actual material and finish. Inspect consumable inserts or film for wear and damage, and replace them according to condition and the supplier's instructions rather than a universal cycle count.
Complete Tooling Selection Guide: Matching Tools to Your Job
Use this decision matrix to quickly identify the correct punch and die combination for any bending job:
| Bending Job | Recommended Punch | Recommended Die | Notes |
|---|---|---|---|
| Simple 90° L-bend | Standard 88° punch | Single V-die; verify opening for the material | Most common setup; air bending |
| Box/channel profile | Gooseneck punch | Single V-die | Check throat depth vs flange height |
| Hemmed edge | Acute 30° punch → flat punch | V-die → hemming die | Pre-bend, then flatten; verify hemming load separately |
| Large radius curve | Radius top punch | Radius die or wide V-die | Multiple light strokes for large radii |
| Z-shaped offset | Offset punch | Offset die (matched pair) | One stroke = two bends; verify offset distance |
| Pre-finished surface | Standard or gooseneck | Mark-free die (urethane inserts) | Check urethane durometer for material thickness |
| Mixed thickness production | Standard punch (matched to thickest) | Multi-V die (4-way) | Rotate die for quick changeover between thicknesses |
Press Brake Tooling Maintenance: Extending Tool Life
Well-maintained tooling produces consistent results and lasts significantly longer. Follow these practices to maximize your tooling investment:
- Clean tooling regularly: Remove metal chips, dust, and debris from the V-groove after each job. Particles trapped between the die and workpiece cause surface marks and accelerate wear.
- Inspect for damage at the intervals specified by the tooling supplier and after an overload or collision. Stop using tools with cracks, chips or deformation and obtain an assessment before returning them to service.
- Lubricate lightly: Apply a thin film of machine oil to die surfaces, especially when bending stainless steel or aluminum. This reduces friction, prevents galling, and extends die life.
- Store properly: Keep tooling in a dry, organized storage rack. Never stack punches or dies directly on each other — the hardened edges chip easily on contact. Use wooden or plastic dividers.
- Never exceed rated tonnage: This is the number one cause of premature tooling failure. Always calculate required tonnage before bending and verify it is within the tool's capacity.
- Align precisely: Misaligned punch and die cause uneven wear on one side. Use alignment gauges and check parallelism when installing tooling. On CNC machines, run the alignment check routine in the controller.
For a complete maintenance program including daily, weekly, and annual tasks, see our Press Brake Maintenance Schedule guide.
Press Brake Tooling Quote Checklist
Tooling selection should be checked against the real machine and drawings. Before asking Rucheng for a tooling recommendation, prepare the information below so the punch, die opening, tooling material and segmentation can be matched correctly.
| Information to send | Why it matters |
|---|---|
| Material grade and thickness range | Controls V-die opening, required tonnage, bend radius and tool steel choice. |
| Part drawings and bend sequence | Shows whether standard, gooseneck, hemming, radius or offset tooling is needed. |
| Press brake model and tooling standard | Confirms clamp compatibility, tool height, safety tang and maximum load. |
| Surface finish requirement | Determines whether mark-free tooling, film, larger V-opening or polished shoulders are needed. |
| Production volume and changeover frequency | Helps choose standard tools, segmented tools, multi-V dies or custom profiles. |
Frequently Asked Questions
Conclusion: Choose the Right Tooling, Get Perfect Bends
Press brake tooling selection is the foundation of accurate, efficient sheet metal bending. Understanding the differences between punch types (standard, gooseneck, acute, radius, sash, offset) and die types (V-die, multi-V, hemming, U-die, Z-die, radius) allows you to match the right tools to every job — reducing setup time, minimizing scrap, and producing consistent parts.
Choose tooling from the part requirements, then verify clamping, clearance and load limits. Opening-to-thickness ratios are starting points for defined materials and methods, not universal settings. Confirm the setup with supplier data and sample bends before production.
Need Press Brake Tooling for Your Shop?
Send your material grade, thickness, bend length, part drawing and machine details. We can review the tooling requirements and prepare a quotation identifying the proposed profiles, materials, clamping interfaces and supply scope.
Request a Press Brake Tooling QuotePress brake selection and production resources
Compare the full Rucheng press brake machine range before choosing tonnage, working length, controller, tooling and automation options.
- Electro-hydraulic CNC press brake for high-mix precision bending.
- Press brake molds and dies for standard punches, V-dies, gooseneck tooling and custom profiles.
- Tandem press brake for long parts, poles, panels and structural work.
- Press brake tonnage calculation, tooling selection and controller selection help confirm the final specification.
- When your drawings are ready, send tooling requirements through the press brake quote form.
- For blank preparation before bending, compare fiber laser cutting machines and plan the cutting-to-bending workflow together.